

Chiller for Chemical Industry

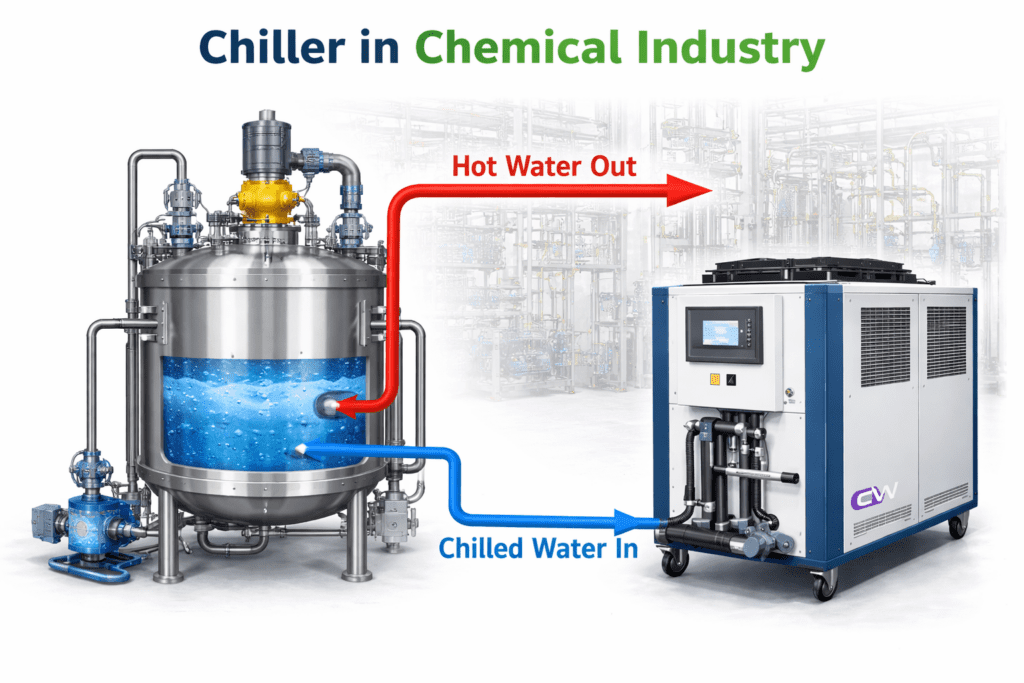
Chiller for Chemical Industry: Complete Guide to Process Cooling, Efficiency & Selection
The chemical industry is one of the most temperature-sensitive manufacturing sectors. Whether it is handling exothermic reactions, solvent recovery, polymer processing, or maintaining product stability, precise temperature control is not optional—it is critical. This is where industrial chillers play a vital role.
A well-designed chiller system ensures consistent product quality, improves process efficiency, reduces downtime, and enhances plant safety. In this detailed guide, we will explore how chillers are used in the chemical industry, their working principle, applications, benefits, and how to select the right system for your plant
🔷 Why Temperature Control is Critical in the Chemical Industry
Chemical processes often involve reactions that either release heat (exothermic) or absorb heat (endothermic). If this heat is not properly controlled, it can lead to:
🔷 Product degradation
🔷 Reduced reaction efficiency
🔷 Equipment damage
🔷 Safety hazards (runaway reactions)
🔷 Increased rejection rates
For example, in a reactor vessel, even a small temperature fluctuation can change the reaction rate, leading to inconsistent product quality. Therefore, maintaining a stable and controlled temperature environment is essential.
This is where chillers provide a reliable and continuous cooling solution.
🧊 Types of Chillers Used in Chemical Industry
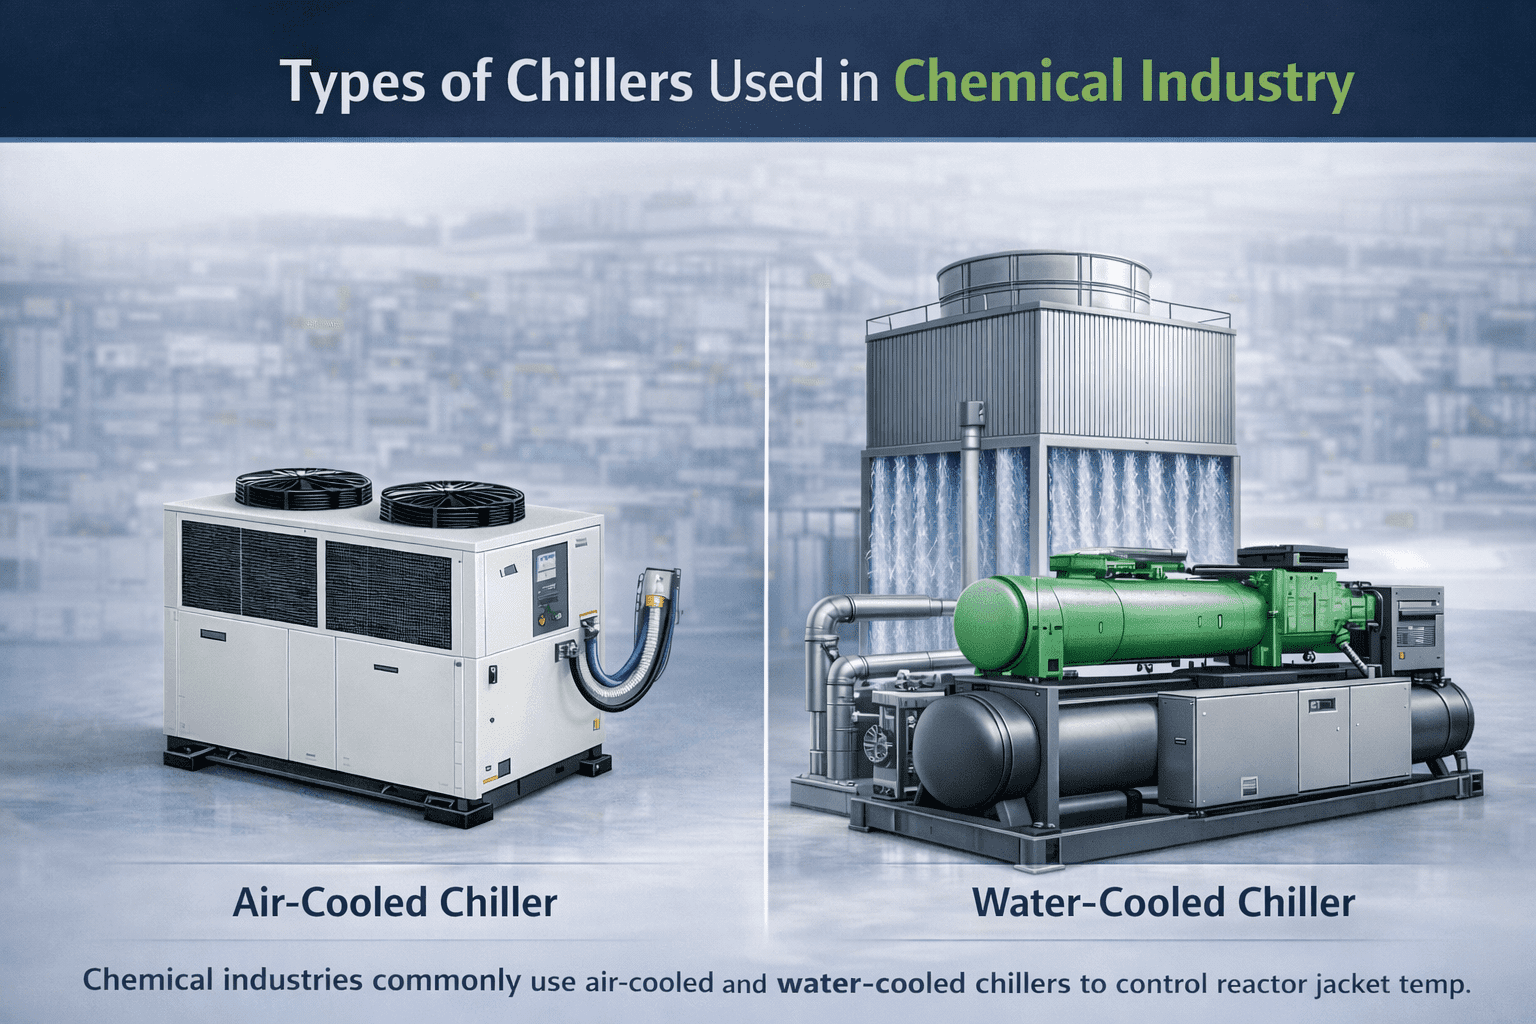
Air-cooled and water-cooled chillers are widely used in the chemical industry for precise and reliable process cooling.
They play a critical role in maintaining stable temperatures, product quality, and GMP compliance
1. Air-Cooled Chillers
These chillers use ambient air to dissipate heat.
🔷 Suitable for small to medium plants
🔷 Easy installation (no cooling tower required)
🔷 Higher operating cost compared to water-cooled systems
🔷 Ideal where water availability is limited
2. Water-Cooled Chillers
These systems use cooling towers for heat rejection.
🔷 Higher efficiency and lower operating cost
🔷 Suitable for large chemical plants
🔷 Stable performance even in high ambient temperatures
🔷 Requires cooling tower and water treatment
3. Brine Chillers (Low Temperature Chillers)
Used when processes require temperatures below 0°C.
🔷 Uses glycol or brine solution
🔷 Ideal for pharmaceutical and specialty chemicals
🔷 Prevents freezing in pipelines
🔷 Supports temperatures as low as -40°C
4. Screw Chillers / Scroll Chillers
Based on compressor type:
🔷 Scroll Chillers – Best for small capacity (10 TR – 60 TR)
🔷 Screw Chillers – Ideal for medium to large capacity (50 TR – 500 TR+)
🧊 Understanding the Chemical Process Chiller System
To understand the importance of a chiller in the chemical industry, it is essential to first understand how chemical manufacturing processes work.
Chemical production typically involves the following stages:
🔷 Raw material handling and preparation
🔷 Chemical reactions (exothermic/endothermic)
🔷 Cooling and temperature stabilization
🔷 Separation, distillation, and purification
Among these stages, temperature control during reaction and cooling is one of the most critical factors.
🔷 Why Temperature Control is Critical in Chemical Industry
During chemical processing, a large amount of heat is generated in reactions, mixing, and heat transfer operations. This heat must be removed efficiently to maintain process safety and stability.
If cooling is slow or inconsistent, several problems can occur:
❌ Uncontrolled or runaway chemical reactions
❌ Degradation of chemicals and raw materials
❌ Variation in product quality and yield
❌ Equipment damage due to overheating
❌ Increased production downtime and operational cost
🔷 Why Chillers Are Important for Chemical Industry
Many small and mid-scale plants initially rely on cooling towers or ambient water systems. While these may provide basic cooling, they cannot deliver the precision, consistency, and reliability required in chemical processes.
A properly designed chemical industry chiller offers several key advantages:
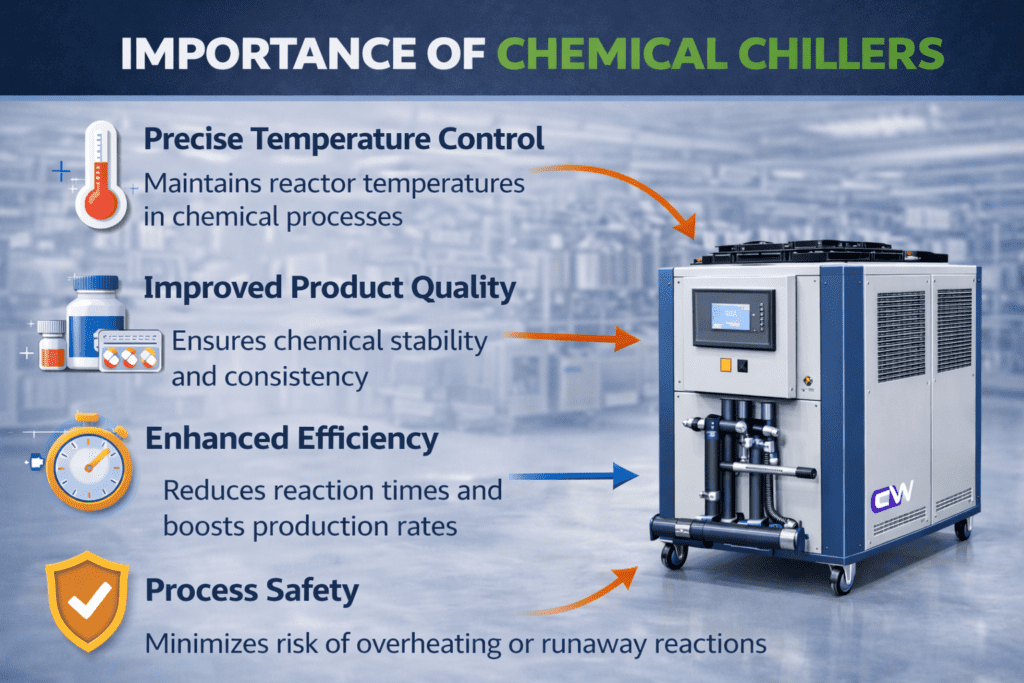
🔹 1. Precise Process Temperature Control
Chemical reactions require accurate and stable temperature conditions.
✅ Maintains controlled temperature during exothermic reactions
✅ Prevents overheating and thermal instability
✅ Ensures safe and efficient process operation
🔹 2. Improved Product Quality & Yield
A chiller ensures uniform and consistent cooling across all process stages.
✅ Enhances product consistency and chemical stability
✅ Improves reaction efficiency and yield
✅ Reduces batch variations and rework
✅ Meets strict pharmaceutical quality standards
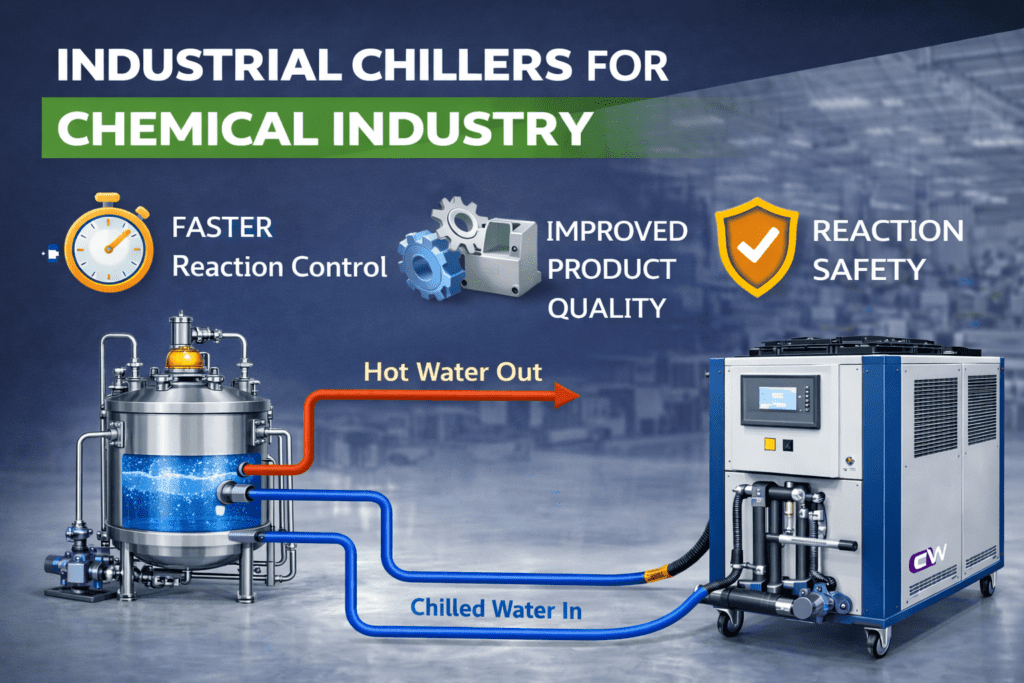
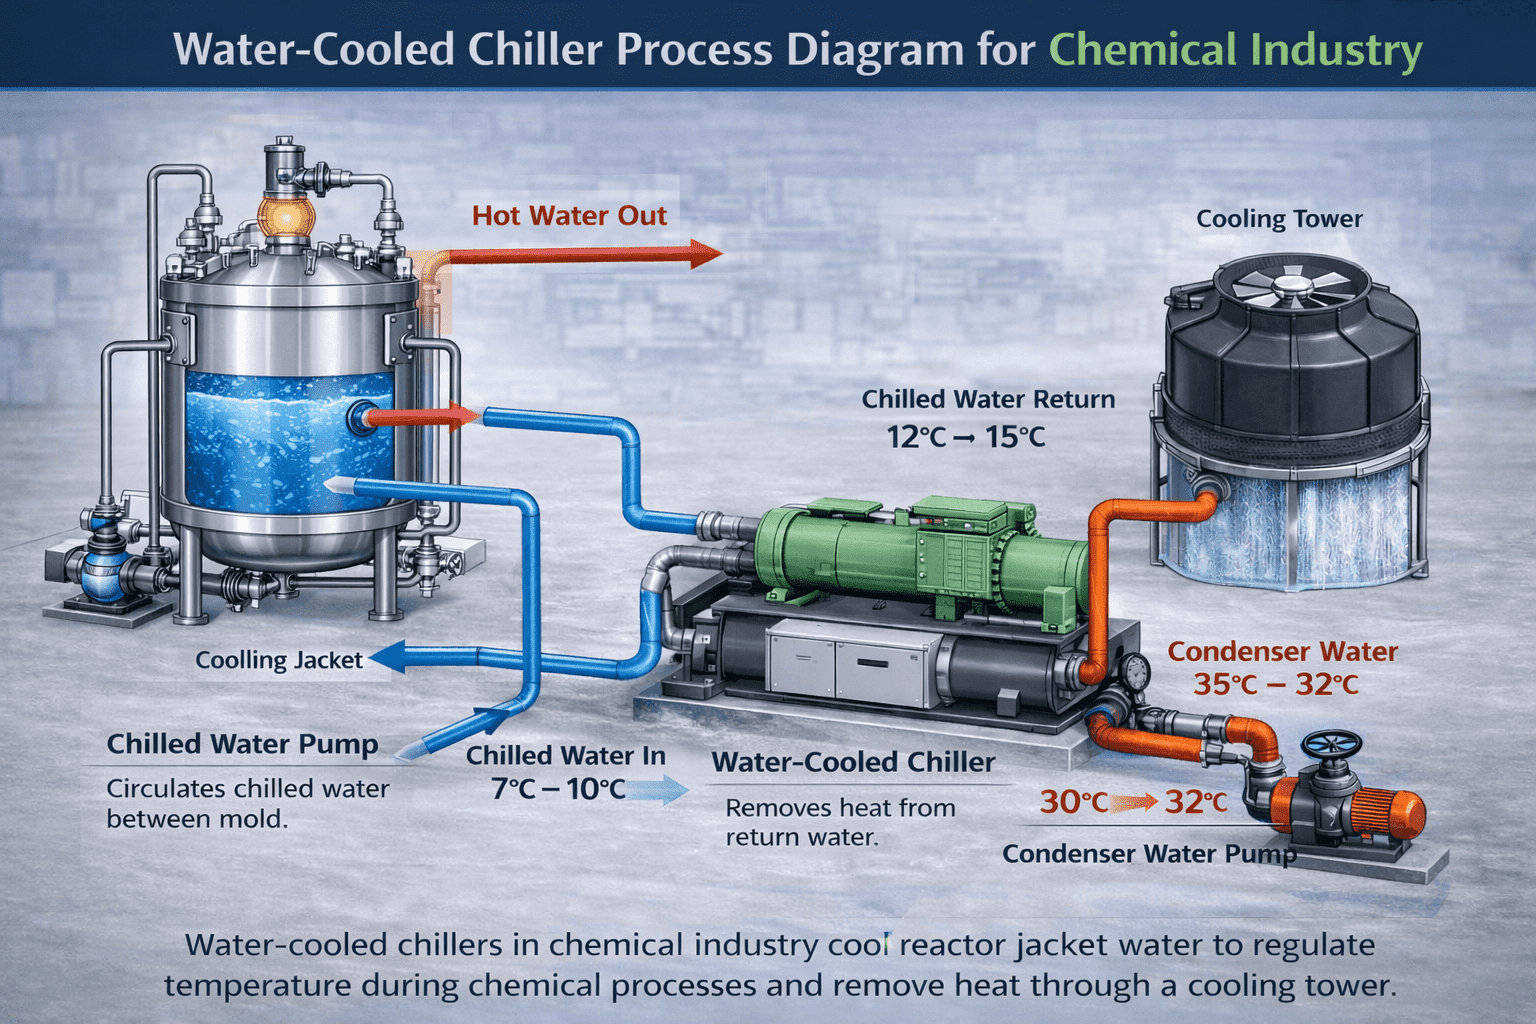
🧊 Process of Chemical Cooling using a Water-Cooled Chiller
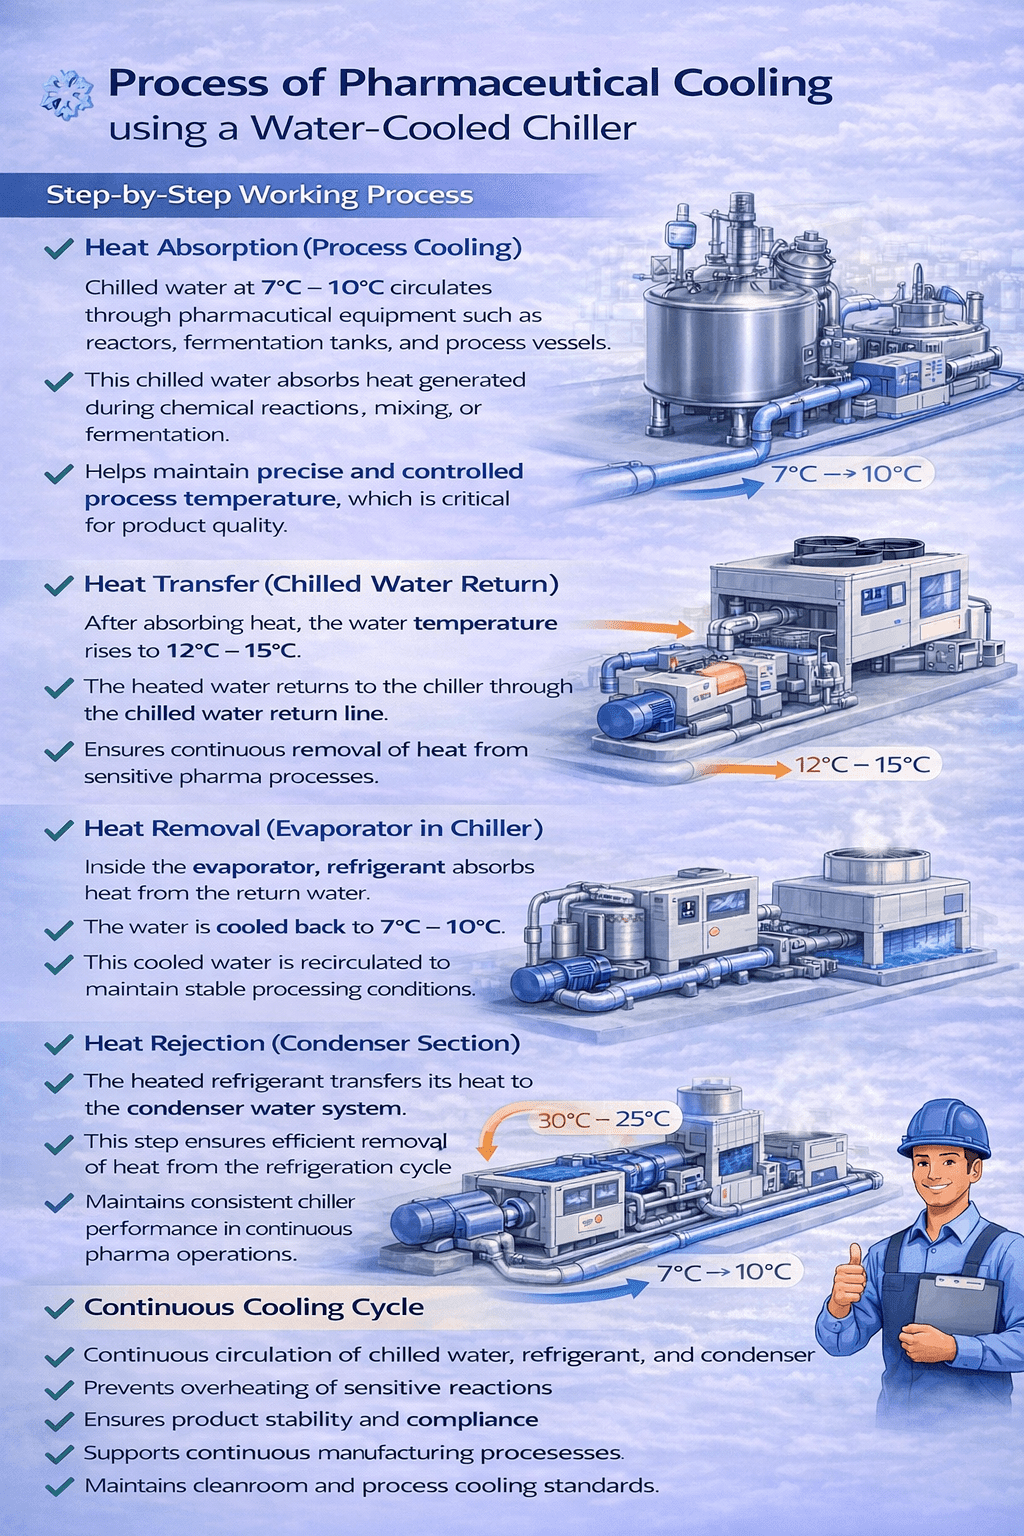
Step-by-Step Working Process
Step-by-Step Working Process
🔹 Heat Absorption (Process Cooling)
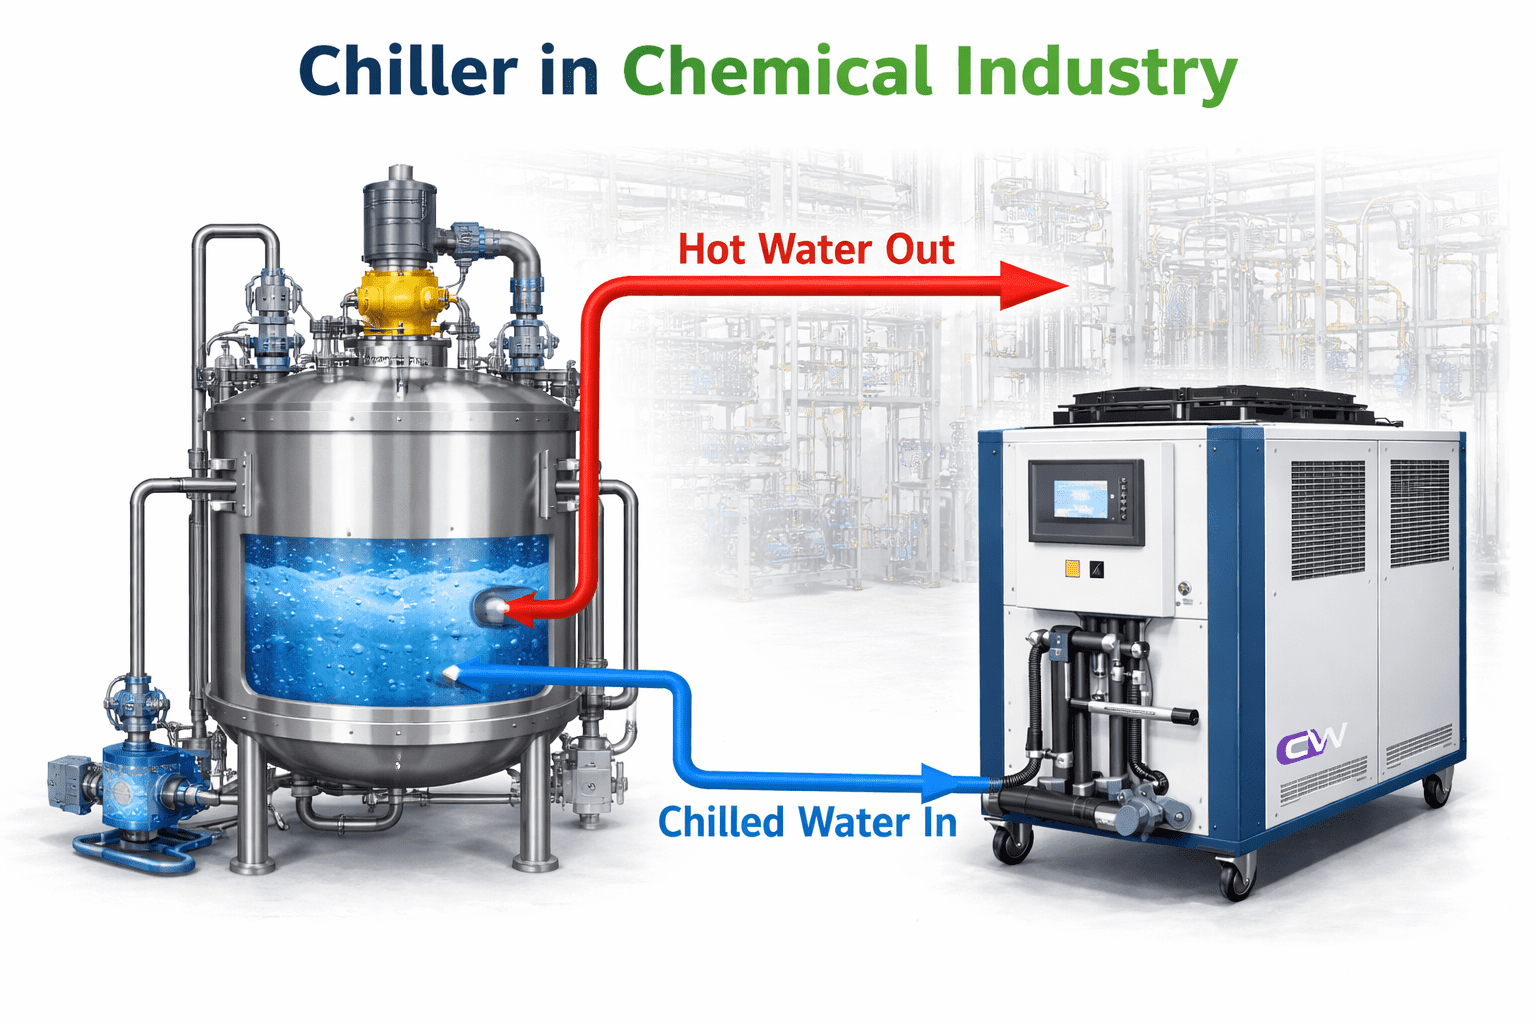
✅ Chilled water at 7°C – 10°C circulates through chemical equipment such as reactors, heat exchangers, distillation units, and process vessels.
✅ This chilled water absorbs heat generated during exothermic reactions, mixing, and heat transfer operations.
✅ Helps maintain precise and controlled process temperature, which is critical for reaction stability and product consistency.
🔹 Heat Transfer (Chilled Water Return)
✅ After absorbing heat, the water temperature rises to 12°C – 15°C.
✅ The heated water returns to the chiller through the chilled water return line.
✅ Ensures continuous removal of heat from chemical processes and equipment.
🔹 Heat Removal (Evaporator in Chiller)
✅ Inside the evaporator, the refrigerant absorbs heat from the return water.
✅ The water is cooled back to 7°C – 10°C.
✅ This cooled water is recirculated to maintain stable chemical processing conditions.
🔹 Heat Rejection (Condenser Section)
✅ The heated refrigerant transfers its heat to the condenser water system.
✅ This step ensures efficient removal of heat from the refrigeration cycle.
✅ Maintains consistent chiller performance in continuous chemical plant operations.
🔹 Cooling Tower Heat Dissipation
✅ The condenser water carrying heat flows to the cooling tower.
✅ Heat is rejected to the atmosphere through evaporation and airflow.
✅ The cooled condenser water returns to the chiller for reuse.
🔹 Continuous Cooling Cycle
✅ Continuous circulation of chilled water, refrigerant, and condenser water ensures:
🔷 Stable temperature control for chemical reactions
🔷 Consistent product quality and process efficiency
🔷 Safe and reliable operation in industrial environments
🔷 Reduced downtime and improved production output
🔥 Key Advantages in Chemical Industry
✅ Prevents overheating and runaway chemical reactions
✅ Ensures stable reaction conditions and product quality
✅ Supports continuous and batch processing systems
✅ Improves equipment life and operational safety
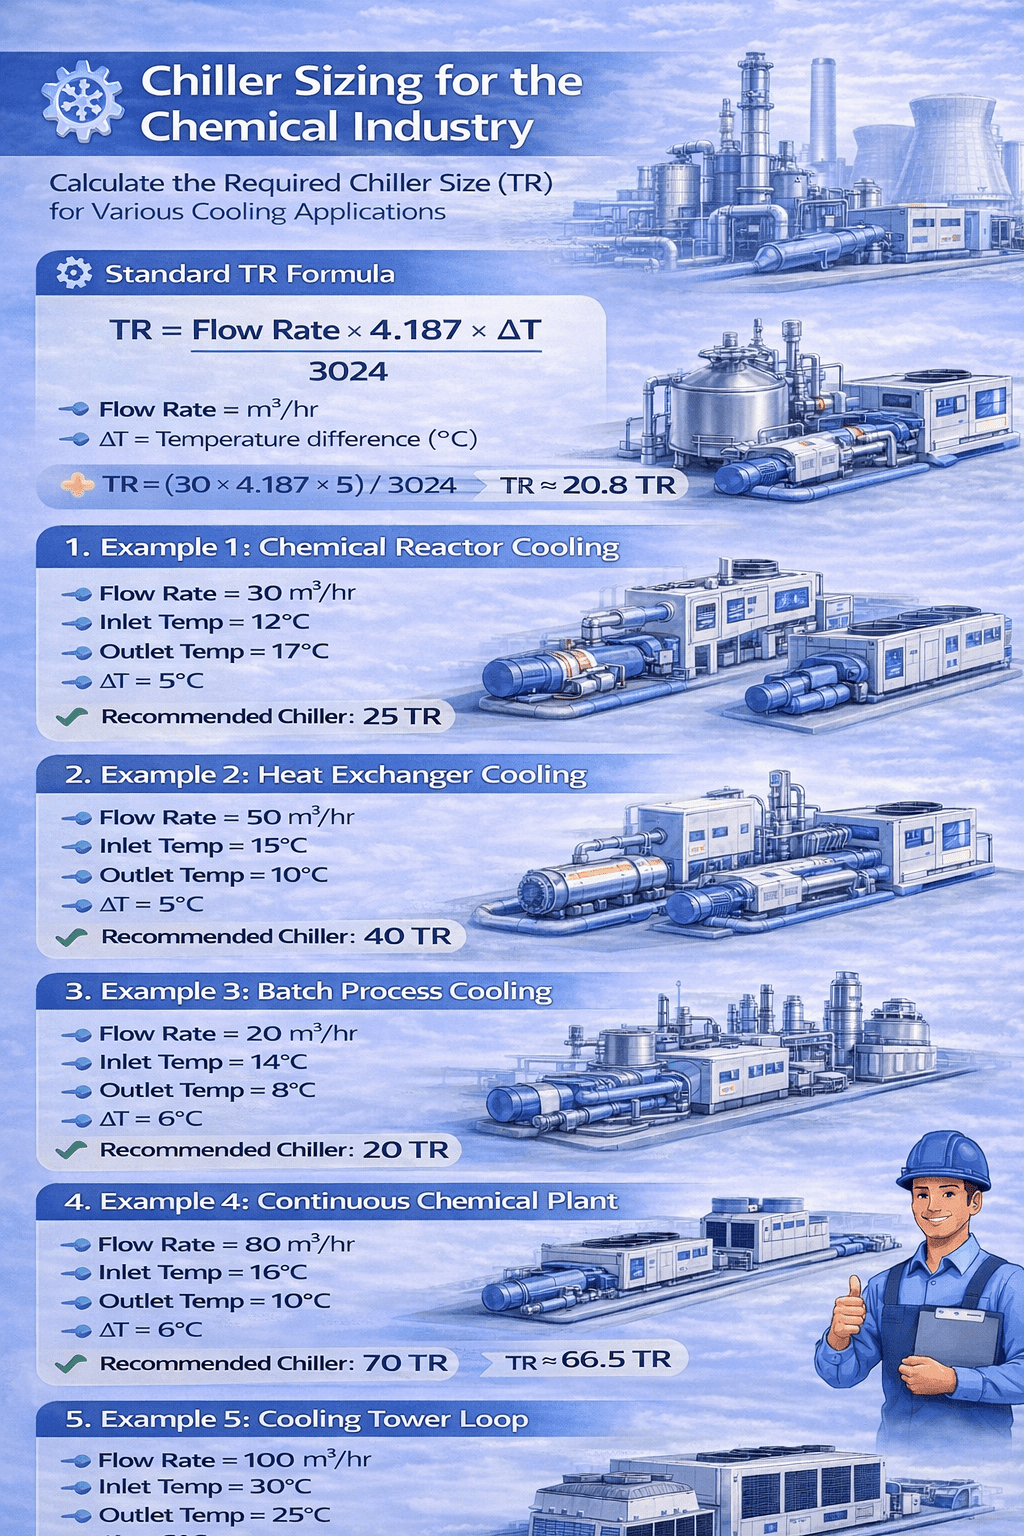
How to Calculate TR for Chemical Chiller (with Example)
🔷 Industry-Standard Formula Section
Use this formula block (center highlight box):
TR=3024Flow Rate×4.187×ΔT
🔷 Practical Example (Chemical Application)
📌 Application:
Cooling for Chemical Reactor & Heat Exchanger Process
🔷 Given Data (Checklist Style)
✔ Water Flow Rate = 30 m³/hr
✔ Chilled Water Inlet Temp = 12°C
✔ Chilled Water Outlet Temp = 7°C
✔ Temperature Difference (ΔT) = 5°C
🔷 TR Calculation Section
TR = (30 × 4.187 × 5) / 3024
TR = 628.05 / 3024
TR ≈ 20.8 TR
👉 Recommended Chiller = 25 TR Chemical Chiller
🔷 Bottom Recommendation Section
✅ A 25 TR Chemical Chiller is recommended to:
• Maintain stable reaction temperature
• Prevent overheating in chemical processes
• Improve product quality and consistency
• Handle continuous plant operation load
• Provide safety margin for future expansion
Request For Free Consultation
Request a Free Consultation from a Leading Chiller Manufacturer
“Get technical consultation from a certified chiller manufacturer and supplier.
We help you select the right chiller system for maximum efficiency and precise temperature control.“
Key Components & Applications
Water-cooled scroll chillers used in the chemical industry are designed for robust performance, process stability, and continuous operation, ensuring reliable cooling for demanding industrial applications.
🔷 Key Components of a Chemical Industry Chiller
A well-designed chemical chiller consists of the following major components:
🔹 Scroll Compressors
✅ High reliability for continuous plant operation
✅ Better part-load efficiency
✅ Smooth and stable capacity control
✅ Reduced risk of process downtime
🔹 Shell & Tube Evaporator
✅ Efficient heat transfer for process cooling
✅ Maintains stable chilled water temperature
✅ Suitable for handling industrial water quality
✅ Easy maintenance and long service life
🔹 Shell & Tube Condenser
✅ High heat rejection efficiency
✅ Works effectively with cooling tower systems
✅ Improves overall system performance
✅ Ensures energy-efficient operation
🔹 Expansion Valve
✅ Precise refrigerant flow control
✅ Maintains stable cooling performance
✅ Protects system from load fluctuations
🔹 Advanced Control Panel
✅ Accurate temperature control (±1°C)
✅ Safety protections and alarm systems
✅ Process monitoring and automation
✅ Energy optimization for cost efficiency
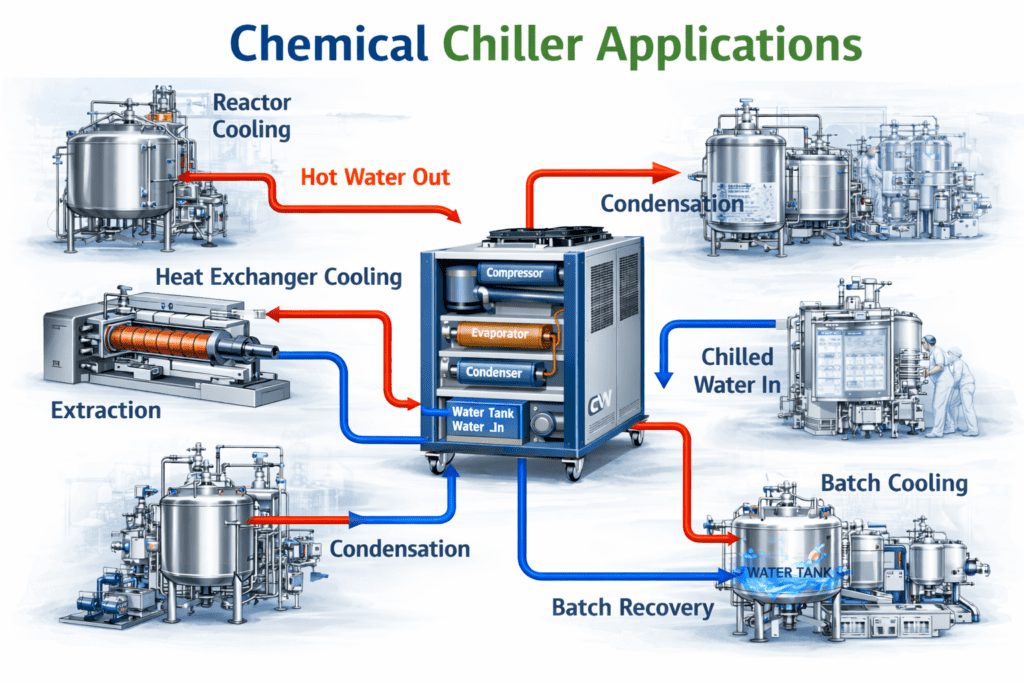
🏭 Typical Applications of Chemical Industry Chillers
Chemical chillers are widely used in applications where temperature control and process stability are critical:
⚗️ Chemical Reactors
✅ Controls exothermic and endothermic reactions
✅ Prevents overheating and runaway reactions
🔥 Heat Exchangers & Process Cooling
✅ Removes excess heat from process fluids
✅ Maintains stable operating conditions
🧪 Batch Processing Systems
✅ Ensures uniform cooling during batch cycles
✅ Improves product consistency and yield
🏭 Continuous Chemical Plants
✅ Supports uninterrupted production processes
✅ Maintains stable temperatures in long operations
🌡️ Distillation & Separation Units
✅ Controls temperature for efficient separation
✅ Enhances purity and process efficiency
🧊 Cooling Tower & Utility Systems
✅ Supports condenser cooling loops
✅ Improves overall plant cooling efficiency
🛢️ Storage Tanks & Chemical Handling
✅ Maintains safe storage temperature
✅ Prevents degradation and volatility of chemicals